Automated control for an explosion-safe production environment
A tailored automation and electrical-engineering project for our European customer, combining ATEX Zone 22 measures, a closed automated waste-handling system, explosion-safe drives and integrated SCADA monitoring.
Safety, automation and control in one integrated system
The project reduced manual intervention around combustible waste handling while improving process visibility and operational control.
Automate a process where safety comes first
Our European customer required a safer and more controlled way to remove combustible waste material from its rice-production process. The existing arrangement needed to be redesigned for an ATEX Zone 22 environment while also improving automation and process visibility.
Minimise explosion risk, reduce manual intervention and create a production environment that could be monitored and controlled locally and remotely.
Three priorities. One integrated solution
Explosion-risk reduction
Implement systems and equipment suitable for the ATEX Zone 22 production environment.
Automated waste handling
Create a closed automated solution for removing waste material without routine human intervention.
Monitoring and data
Use SCADA to monitor and manage the process locally and remotely while collecting operational data.
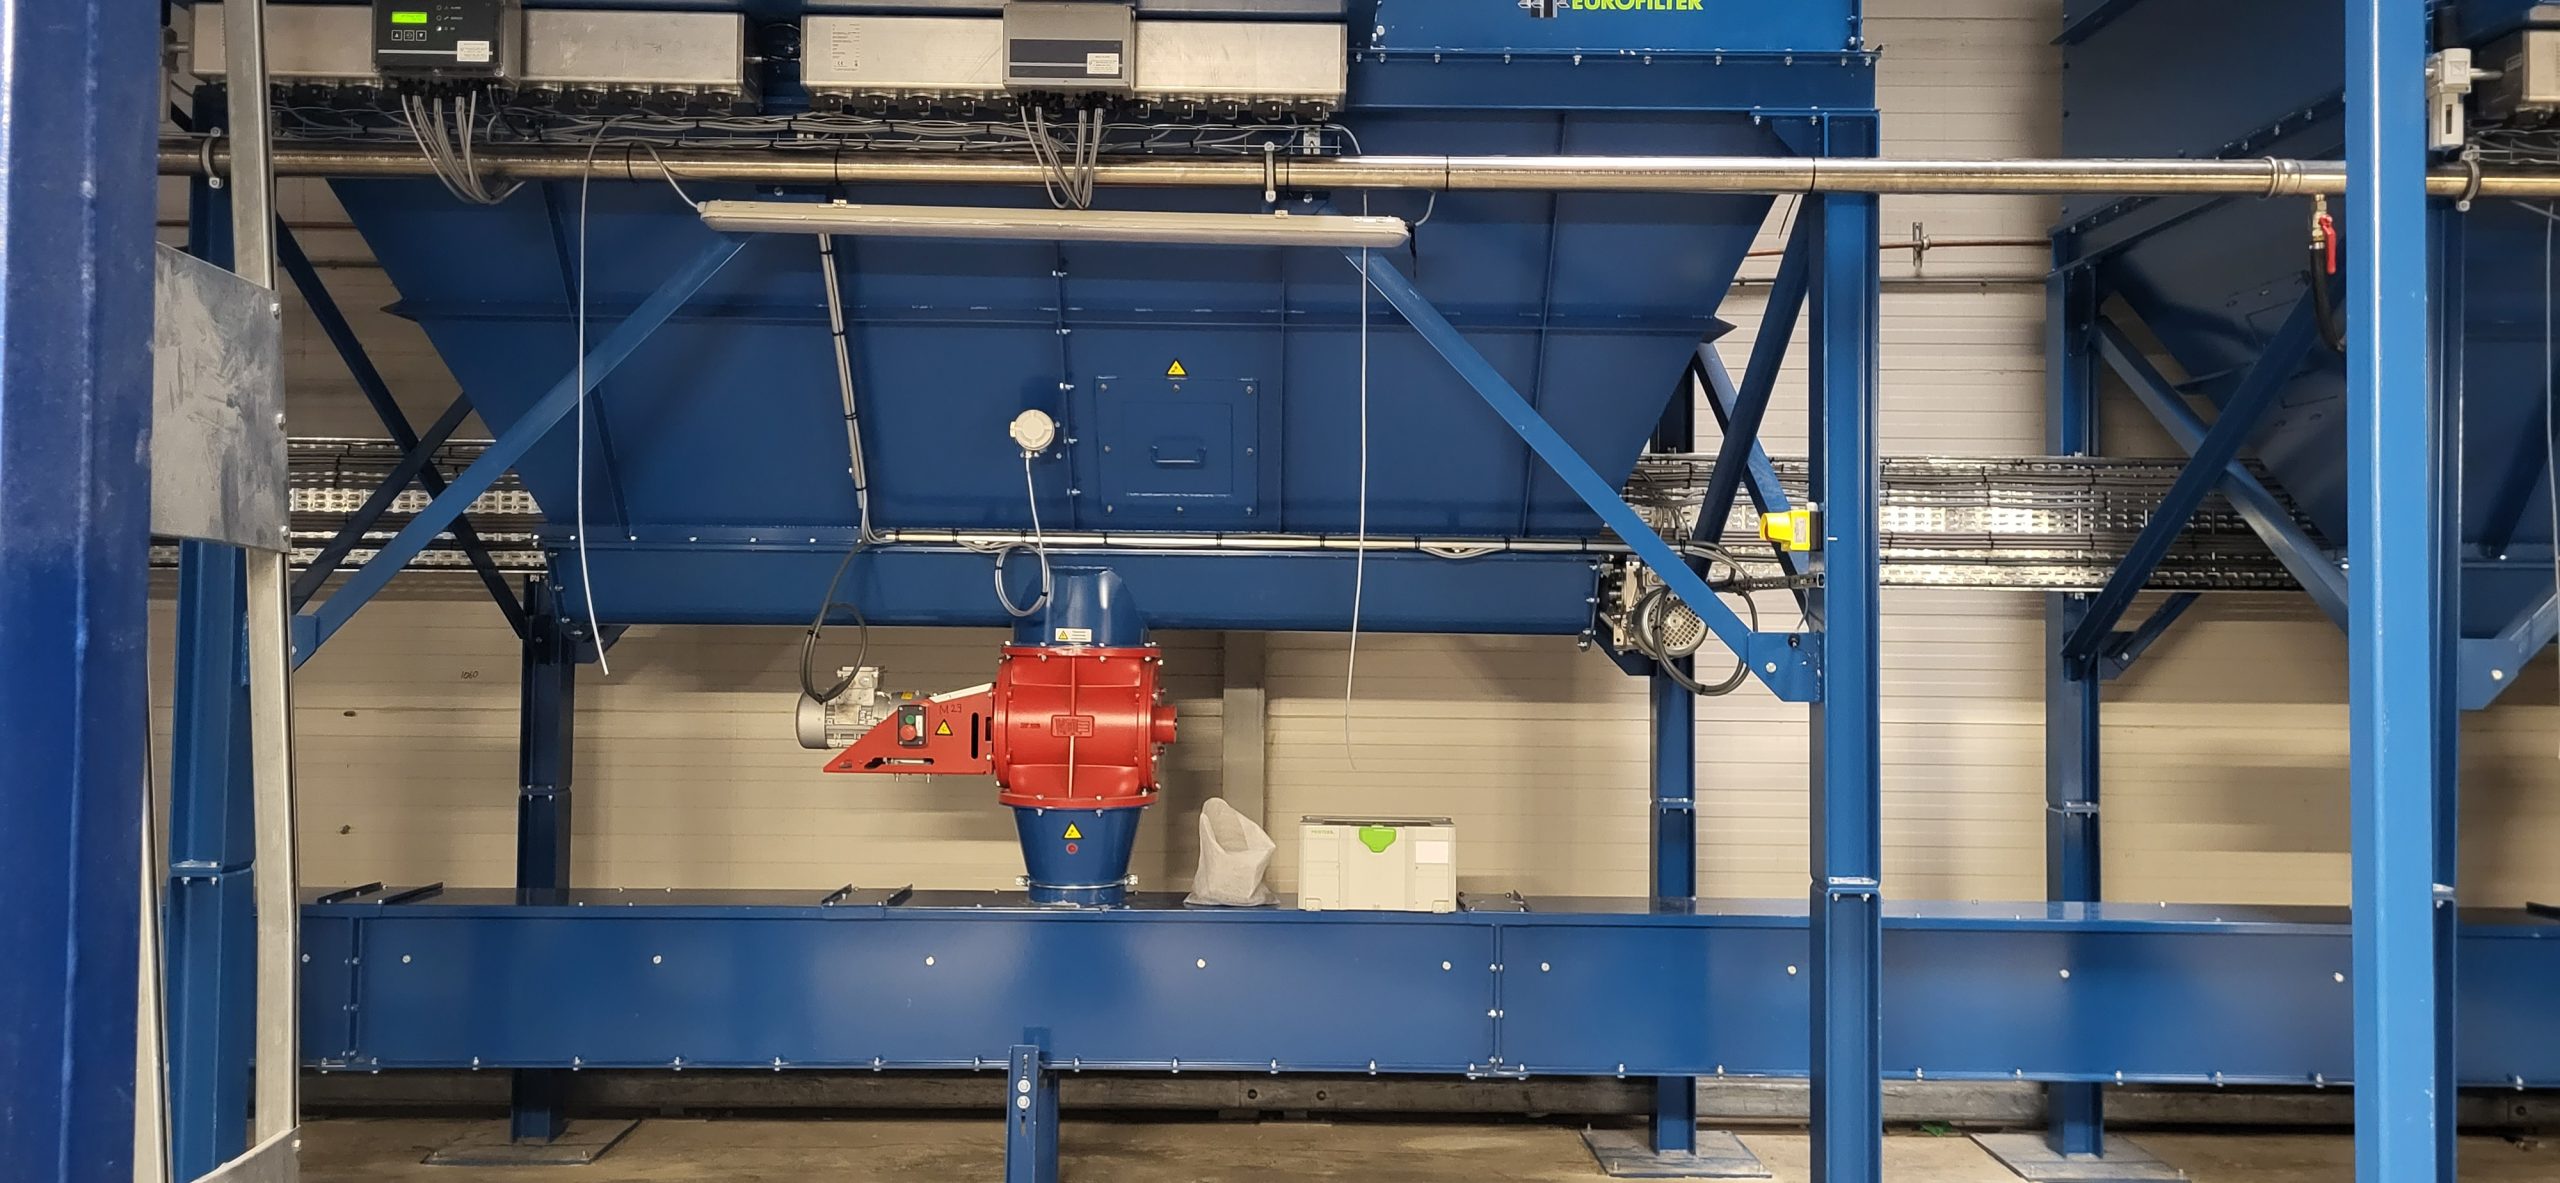
From existing system to automated closed handling
The existing waste-removal system was comprehensively revised and replaced by an automated, fully closed solution. This enabled combustible waste material to be removed more efficiently while supporting the ATEX Zone 22 concept.
Electrical and controls engineering for the complete system
The work covered the physical handling system, electrical infrastructure, explosion-safe drives and the control and monitoring layer.
Automated waste-discharge system
The existing discharge system was redesigned as a fully closed automated arrangement for handling combustible production waste.
ATEX-compliant electrical systems
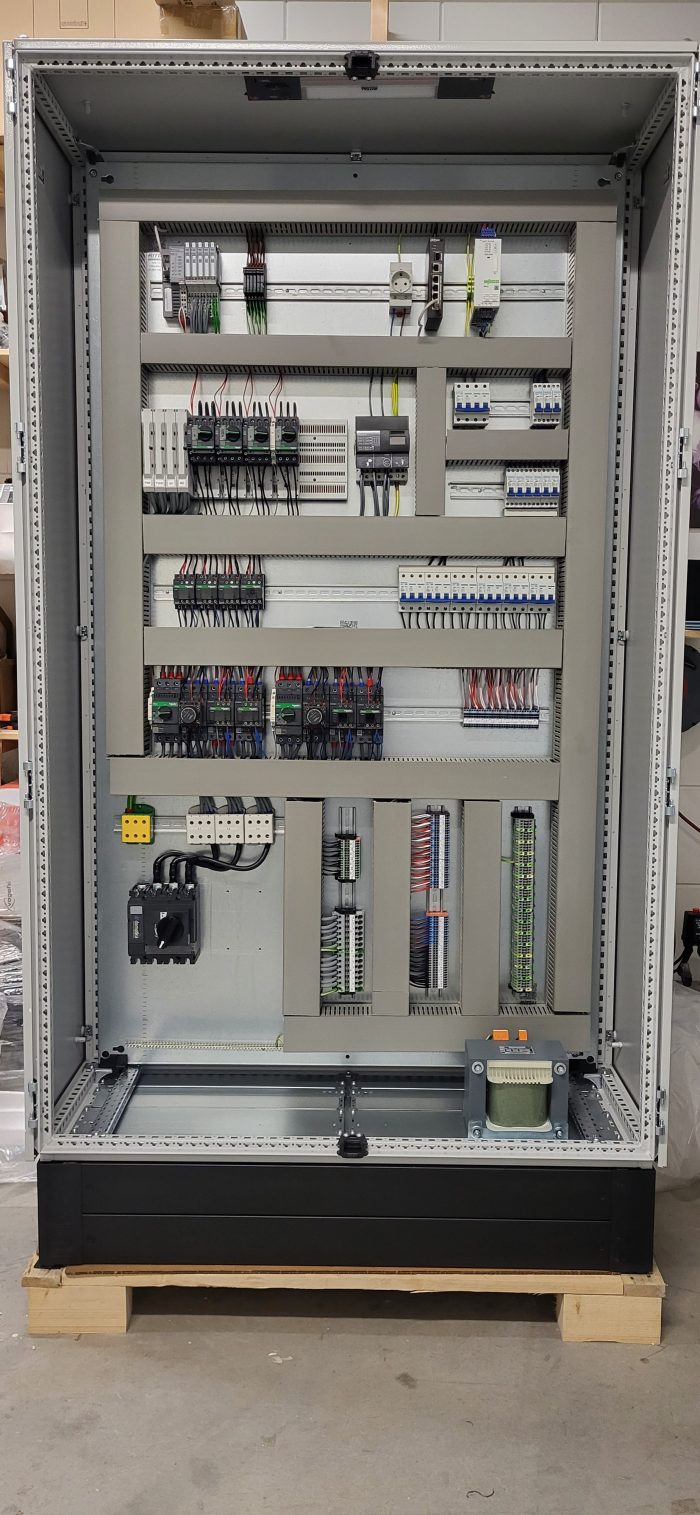
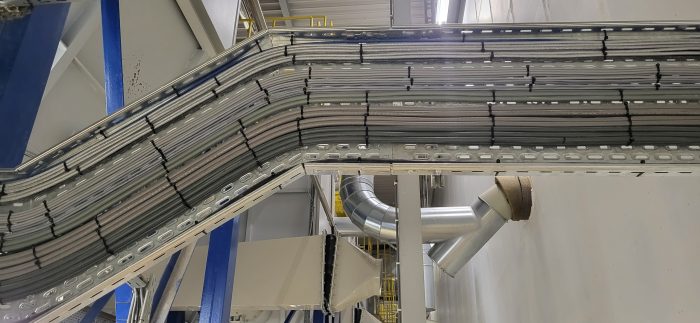
Electrical installation work, including cabling, control cabinets and sensors, was engineered around the applicable ATEX EX requirements stated for the project.
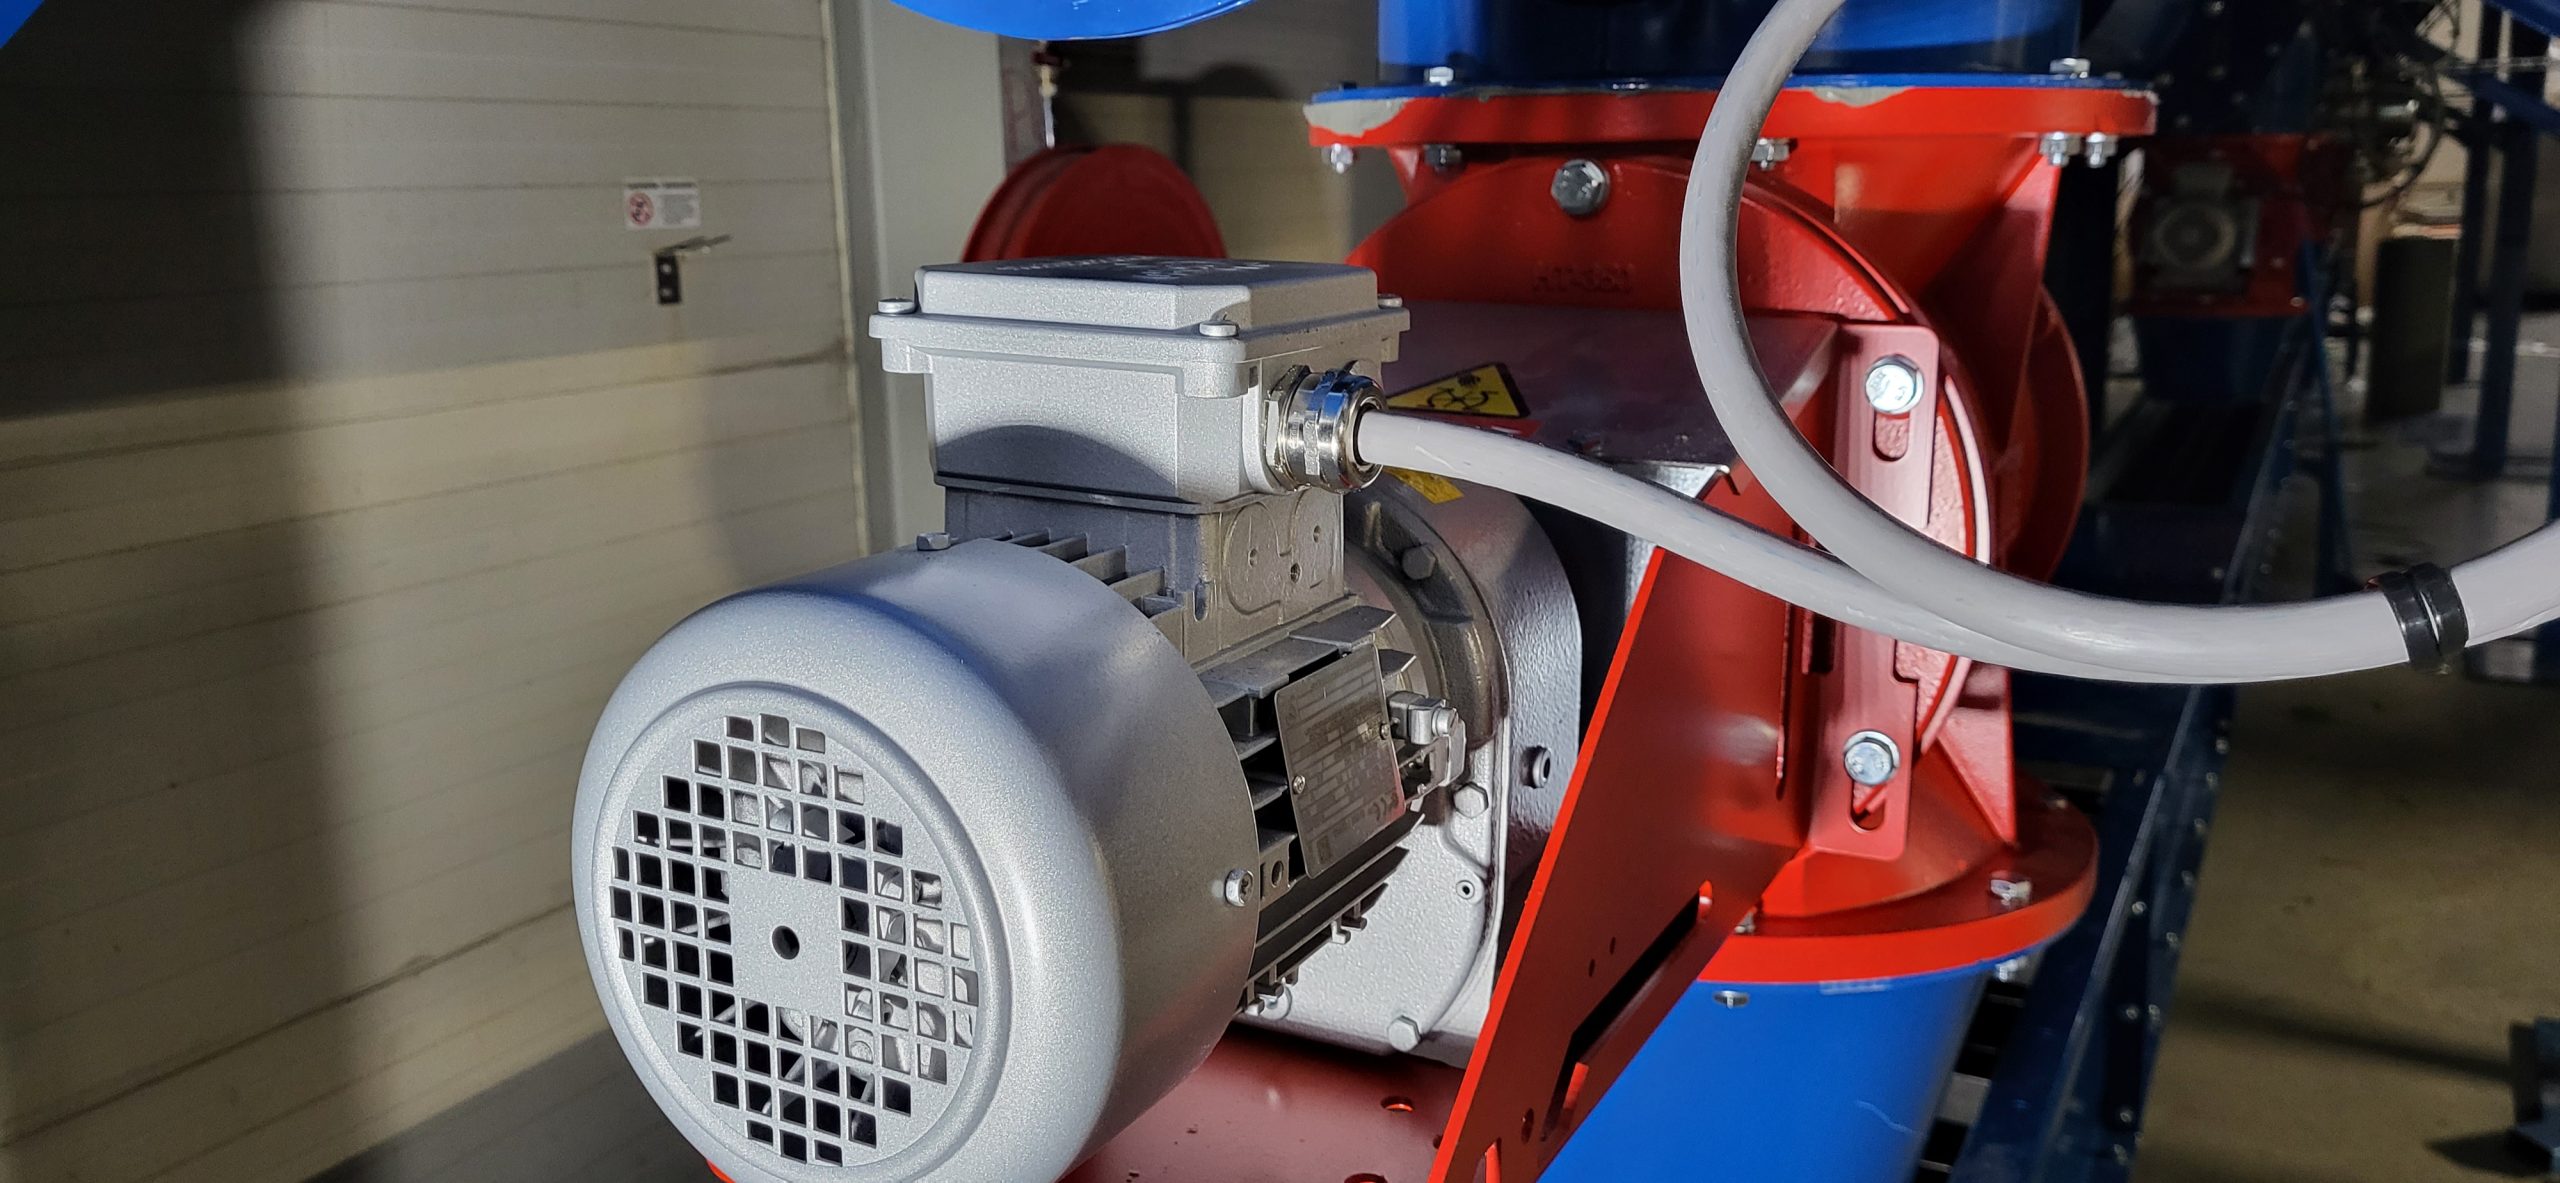
Explosion-safe motors
Special explosion-safe motors were installed to drive conveyor equipment used in the process.
SCADA integration
A SCADA interface was implemented for real-time control and monitoring, both locally and remotely, together with data collection, processing and storage.
Equipment selected for the production environment
Explosion-safe motors form part of the engineered solution for moving material through the waste-handling process.
Engineered cabinets, cabling and control architecture
The project included the control cabinets, cabling and sensor infrastructure needed to automate the process and connect it to the supervisory control layer.
Safer operation with better process control
The completed system improved safety, efficiency and control in the production environment.
Reduced explosion risk
ATEX-compatible equipment and a closed automated process reduced exposure to risks associated with combustible production waste.
Less manual intervention
Automated waste handling reduced routine manual involvement in the process.
Integrated visibility
SCADA provided local and remote monitoring together with operational data collection.
Need to automate a demanding production environment?
Talk to Manomay about combining controls, electrical engineering, process automation and monitoring into one practical industrial solution.
Discuss your project →